 English
 lugha ya Kiswahili
 Монгол хэл
 Español
 Português
 русский
 Français
 日本語
 Italiano
 한국어
 Malay
 हिन्दी
 Türkçe
 العربية
 Indonesia
 تمل
 український
 فارسی
 Latine
 Azərbaycan

Products


Purlin Roll Former
As a important building frameworks to support roofs and walls, purlins features light weight and durable. Advanced purlin roll former often incorporate features like automated size adjustments, material feeding, and punching capabilities, enhancing their versatility and productivity.
Send Inquiry
Product Description
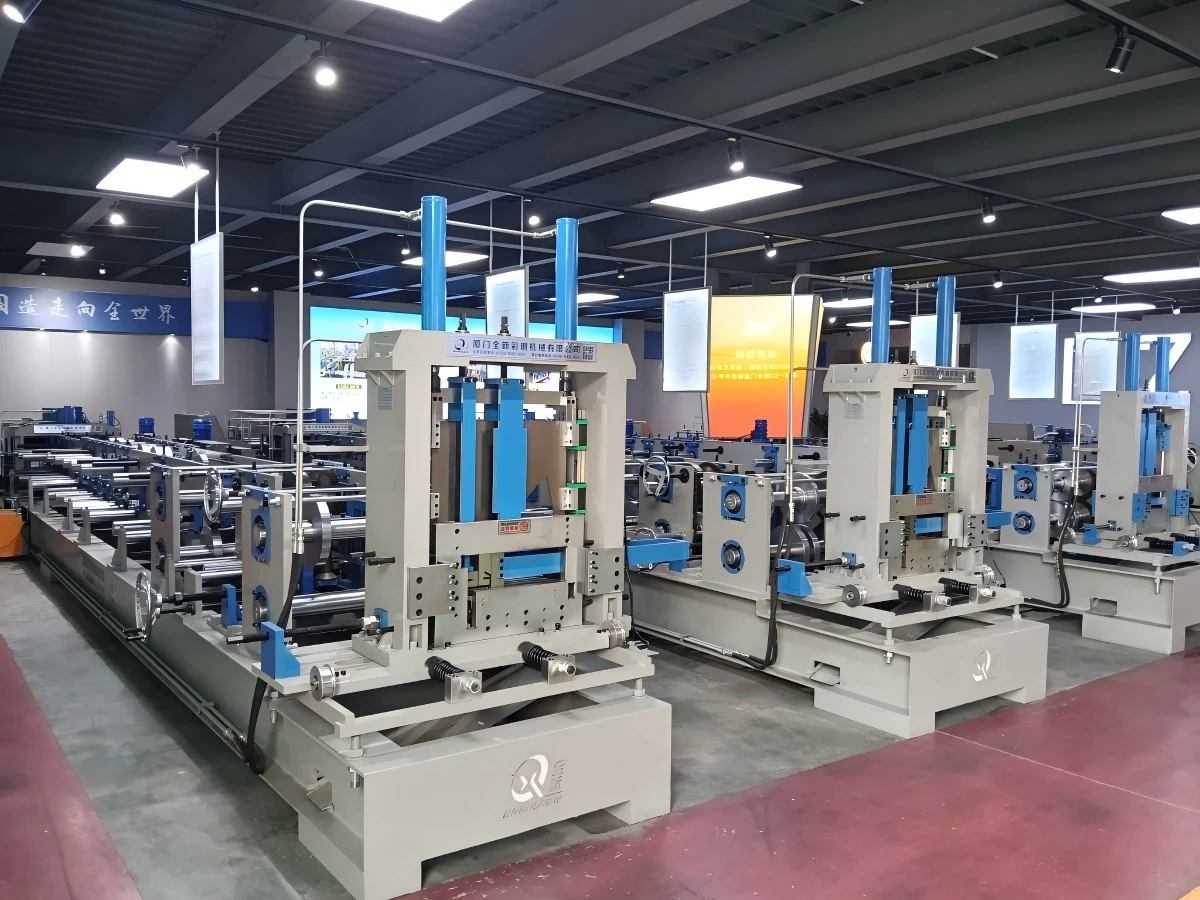
Purlin Roll Former is an automatic roll forming machine used to continuously manufacture steel C purlins, Z purlins, and other structural purlin profiles from metal coils. Beenew purlin roll forming machines can integrate leveling, feeding, punching, roll forming, cutting, and PLC control, with machine configurations customized according to the purlin profile, material thickness, hole pattern, and production requirements.
Beenew's standard purlin roll former configuration supports approximately 1.0–4.0 mm material thickness, 125–422 mm feeding width, 13-20 forming stations, a 70-95 mm shaft diameter, and an 11 kW-30kw driving motor. The actual machine configuration is customized according to the customer's product drawing and steel specifications.
Purlin Roll Former Specifications
|
Item |
Standard Configuration |
|
Machine Type |
Purlin Roll Former |
|
Products |
C / U Purlins |
|
Material Thickness |
1.0–4.0 mm |
|
Feeding Width |
125–422 mm |
|
Forming Stations |
13-20 |
|
Driving Motor |
11-30 kW |
|
Hydraulic Station |
5.5 kW |
|
Shaft Diameter |
70-95 mm |
|
Roller Material |
45# steel, GCR15,GCR12,heat-treated, hard chrome coated |
|
Control System |
PLC + HMI |
|
Punching |
Hydraulic punching, customized |
|
Cutting |
Hydraulic / post-forming cutting |
The above values describe a standard Beenew purlin roll former configuration. Final specifications depend on the customer's purlin drawing, material thickness, steel grade, production speed, punching requirements, and finished dimensions.
What Is a Purlin Roll Former?
A purlin roll former is a continuous cold roll forming machine that converts flat steel coils into structural purlins with a predetermined cross-sectional shape.
The machine gradually bends the steel through multiple forming stations instead of forming the complete profile in a single operation. This progressive forming process allows the machine to produce consistent C, Z, or other customized purlin profiles in continuous lengths.
Purlins are commonly used as secondary structural members in steel warehouses, workshops, industrial buildings, agricultural buildings, roofing systems, and other steel structures.
What Purlins Can a Purlin Roll Former Produce?
Depending on the machine design, a purlin roll former can produce several structural profiles.
C Purlin
C purlins have a C-shaped cross section and are commonly used for structural framing, roof systems, wall systems, and secondary steel members.
Z Purlin
Z purlins have a Z-shaped cross section and are frequently used in steel building roof and wall structures where overlapping purlin connections are required.
C and Z Interchangeable Purlin
A C/Z interchangeable purlin roll forming machine is designed to produce both C and Z profiles from one production line.
This type of machine can reduce duplicate equipment investment when a manufacturer needs to produce multiple purlin profiles.
How Does a Purlin Roll Former Work?
The complete production process normally follows:
Coil Loading → Leveling → Feeding → Punching → Roll Forming → Cutting → Finished Purlin
1. Coil Loading
The steel coil is loaded onto the uncoiler and introduced into the production line.
2. Leveling and Guiding
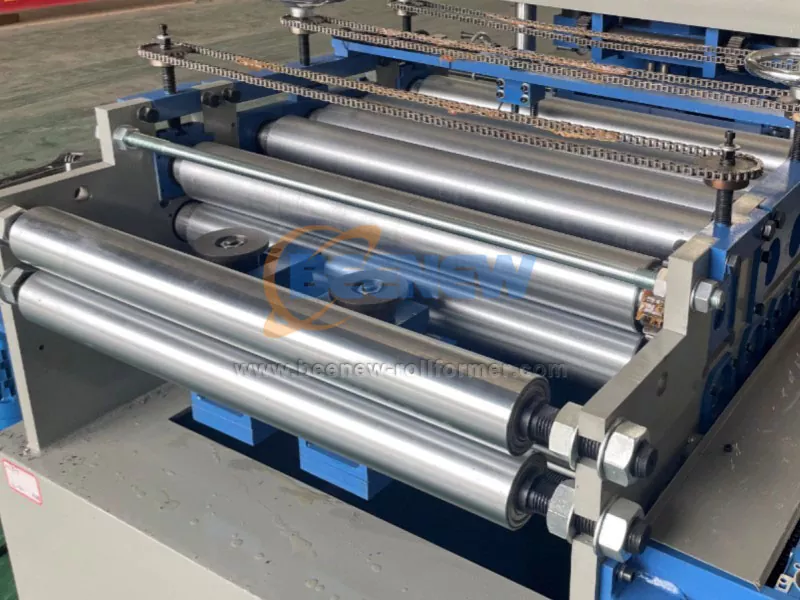
The leveling system removes material deformation and guides the steel strip into the forming section.
Beenew's standard configuration uses a leveling structure with three upper and four lower leveling rollers to improve material alignment before forming.
3. Punching
If the purlin requires connection holes, a hydraulic punching unit can create the specified hole pattern.
The number and configuration of punching dies can be customized according to the customer's production requirements.
4. Roll Forming
The steel strip passes through multiple forming stations.
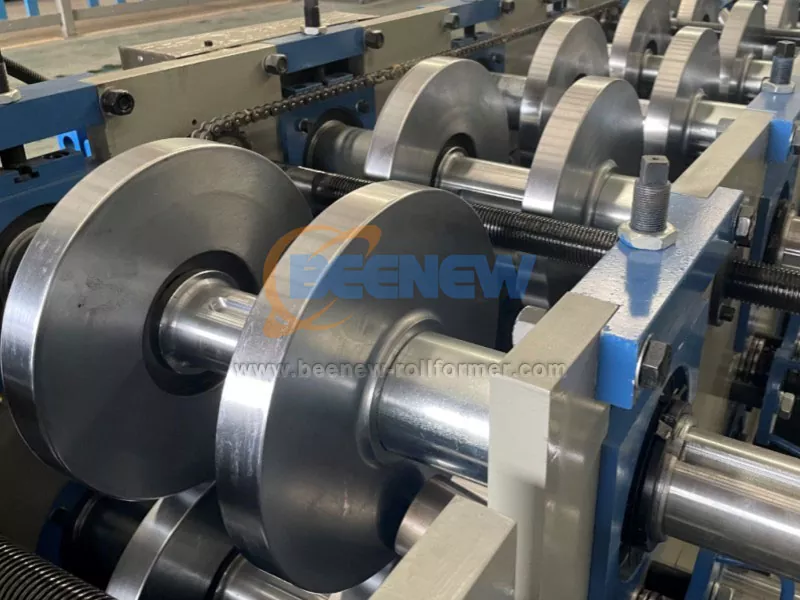
The standard Beenew purlin roll former uses 13 forming stations, with solid shafts and rollers that are precision processed for continuous production.
5. Cutting
After forming, the finished purlin is cut to the programmed length.
Beenew's purlin roll former uses a post-forming universal cutting system, with adjustable blade width and height to accommodate the required profile.
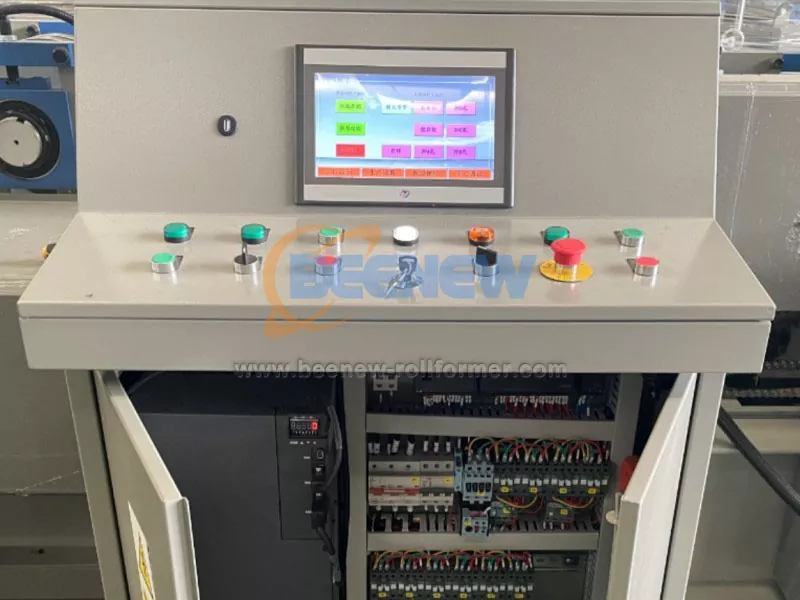
6. PLC Control
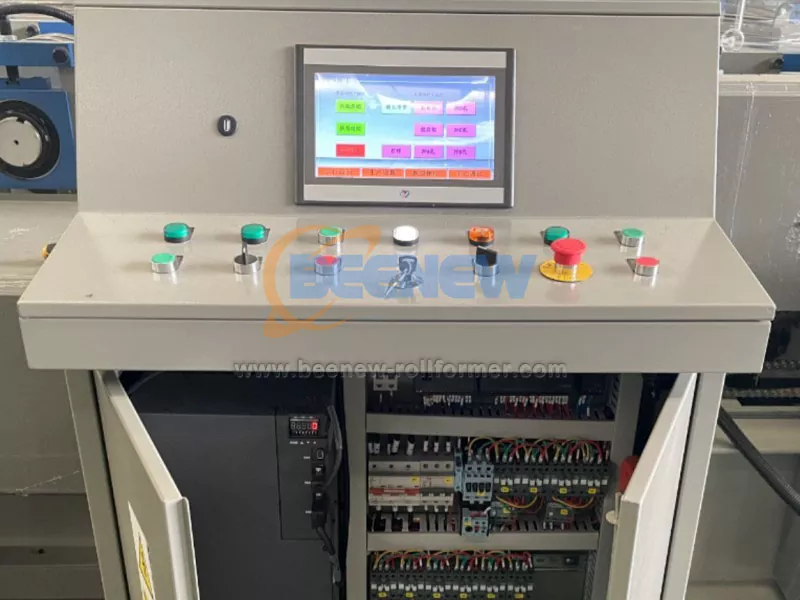
The PLC and HMI system allows the operator to set production parameters such as product length and quantity.
The control system can also display machine operating status and fault information, allowing the operator to monitor the production process from the control panel.
C Purlin vs Z Purlin: Which One Should You Produce?
The choice between C and Z purlins depends on the structural design and connection requirements of the project.
Feature
C Purlin
Z Purlin
Cross Section
C-shaped
Z-shaped
Typical Use
Roof and wall framing
Roof and wall framing
Connection
End-to-end / bolted
Can overlap at supports
Production
Dedicated or adjustable machine
Dedicated or adjustable machine
Multi-Profile Production
Available
Available
For manufacturers producing both profiles, a C/Z interchangeable purlin roll former can provide greater production flexibility than purchasing two completely separate machines.
What Materials Can a Purlin Roll Former Process?
Purlin roll forming machines are normally designed for steel coils suitable for cold roll forming.
Common materials include:
Galvanized steel
Carbon steel
Pre-painted steel
Structural steel strip
The correct material thickness and steel grade must be confirmed before machine design because material properties directly affect roller design, machine strength, motor power, punching force, and forming performance.
For the standard Beenew configuration, the published material thickness range is 1.5–2.0 mm. Other thickness ranges can be engineered for specific purlin applications.
Purlin Roll Former with Automatic Punching
Many steel purlins require holes for bolted connections.
A punching system can therefore be integrated into the roll forming line.
The punching pattern can be customized according to:
Hole diameter
Hole position
Hole spacing
Number of holes
Web holes
Flange holes
Product length
Providing the manufacturer with the actual punching drawing before machine design helps ensure that the punching system matches the finished purlin requirements.
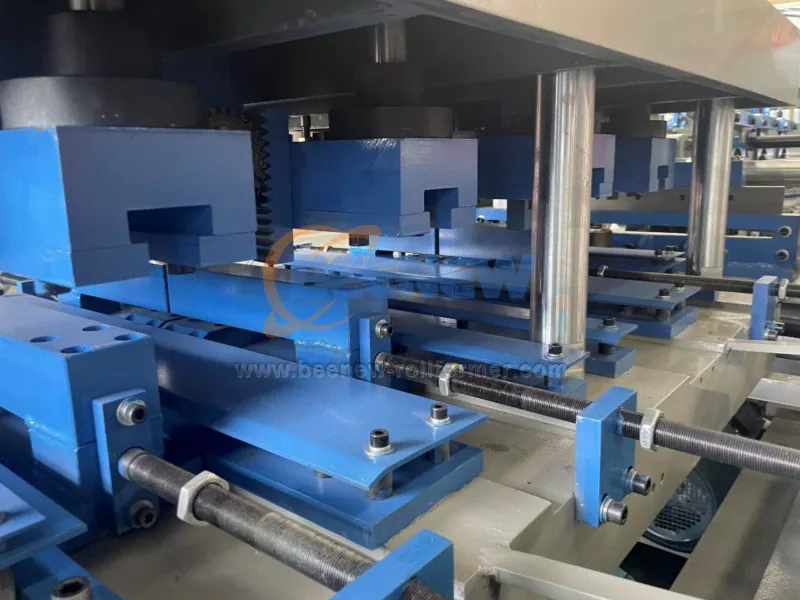
Automatic Purlin Roll Former
An automatic purlin roll former combines several production processes into one controlled line.
A typical configuration includes:
Uncoiler → Leveling → Guiding → Punching → Roll Forming → Cutting → Run-Out Table
The PLC system allows operators to input production parameters through the HMI.
For example, the operator can set the required purlin length and quantity, after which the machine can automatically execute the programmed production cycle.
Adjustable Purlin Roll Former
When a manufacturer needs to produce multiple purlin dimensions, adjustable tooling can provide greater flexibility.
Important adjustable dimensions may include:
Purlin web height
Flange width
Lip size
Material thickness
Punching position
For buyers considering automatic size adjustment, the manufacturer should confirm the actual available size range rather than simply describing the machine as “fully automatic.”
Purlin Roll Former Applications
Purlins produced by roll forming machines are widely used in structural steel applications.
Steel Warehouses
C and Z purlins are commonly used as secondary members supporting roof and wall systems in steel warehouses.
Industrial Buildings
Factories and workshops can use roll-formed purlins for lightweight structural framing.
Agricultural Buildings
Purlins are also used in barns, storage buildings, farm workshops, and agricultural structures.
Roofing Systems
Purlins provide support for roofing panels and transfer loads to the primary structural frame.
Commercial and Construction Projects
Customized purlins can be manufactured according to project-specific structural drawings and installation requirements.
How to Choose a Purlin Roll Former?
Choosing a purlin roll former should begin with the finished purlin profile, not simply the machine name.
Before requesting a quotation, prepare the following information.
1. Purlin Profile Drawing
Provide a dimensioned C or Z purlin drawing showing:
Web height
Flange width
Lip height
Thickness
Bending angles
Hole locations
2. Material Thickness
Specify the exact material range you need.
For example:
1.0 mm / 1.5 mm / 2.0 mm / 2.5 mm / 3.0 mm / 4.0 mm
3. Steel Grade
Specify the required steel grade because different grades can have significantly different forming requirements.
4. Production Speed
Tell the manufacturer your target production output rather than selecting a machine only by advertised maximum speed.
5. Punching Requirements
Provide the complete hole drawing if automatic punching is required.
6. Product Length
Specify whether you need fixed lengths such as 6 m or customized lengths.
7. Number of Purlin Sizes
If you produce several C or Z sizes, tell the manufacturer all required dimensions before machine design.
Purlin Roll Former Price
The price of a purlin roll former depends on the machine configuration and production requirements.
The major cost factors include:
Purlin profile
Material thickness
Steel grade
Forming speed
Number of forming stations
Punching system
Cutting system
Automatic size adjustment
C/Z interchangeable tooling
Motor and transmission system
PLC and electrical components
Uncoiler capacity
Automation level
A machine designed for one fixed C purlin profile will normally have a different configuration and price from a fully adjustable C/Z purlin production line.
For an accurate quotation, send the manufacturer your profile drawing, material specification, required dimensions, punching pattern, finished length, and production target.
Why Choose Beenew Purlin Roll Former?
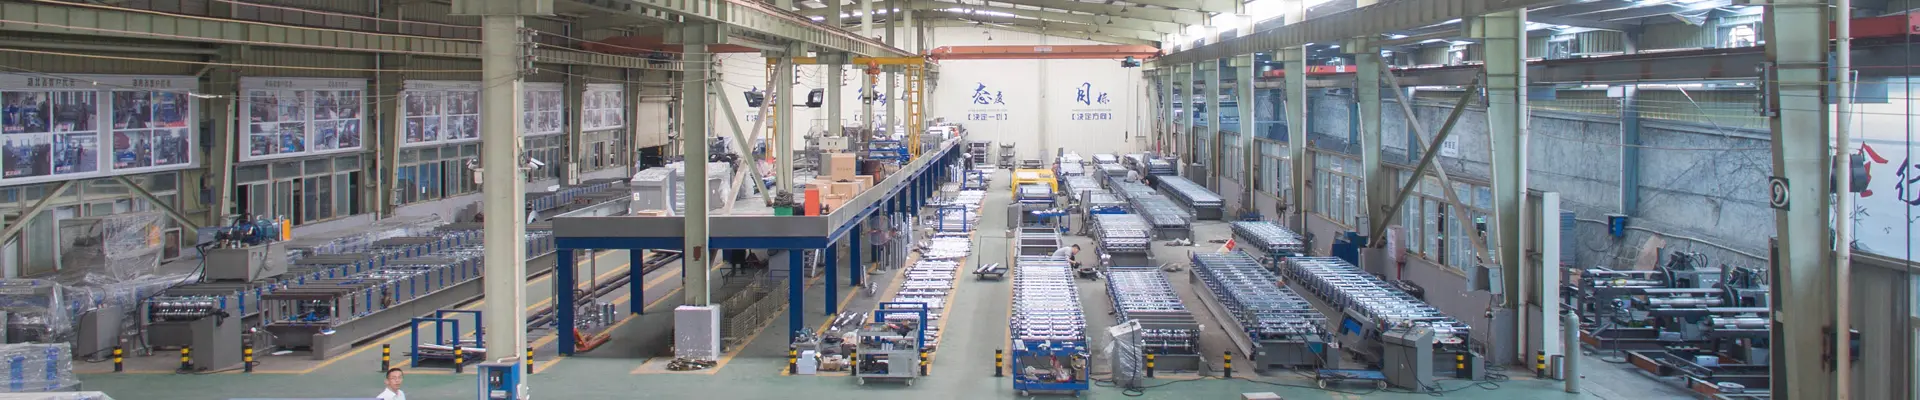
Beenew Machinery is a professional roll forming machine manufacturer based in Xiamen, China, backed by a manufacturing factory established in 1997.
The factory covers approximately 30,000 m² and has more than 200 employees, with an annual production capacity of more than 1,000 roll forming machines. Beenew reports nearly 300 users in 50 countries and has developed patented technologies covering areas such as C/Z interchange, automatic changeover, feeding, transmission, cutting, shearing, and leveling systems.
Beenew's purlin product range includes:
C/Z Purlin Roll Forming Machine
Adjustable Purlin Roll Former
Customized Purlin Roll Forming Machine
The machines can be customized according to the customer's profile drawing, material thickness, hole pattern, finished length, production speed, and automation requirements.
Purlin Roll Former Quality Control
A purlin machine should be tested according to the actual production requirements before shipment.
The recommended factory testing process includes:
1. Machine assembly inspection
2. Electrical system inspection
3.Empty-load machine testing
4. Material feeding test
5. Roll forming test
6. Punching test
7. Cutting test
8. Finished profile measurement
9. Continuous production test
10. Final inspection before shipment
For customized machines, buyers should request a test using the actual profile drawing and material specification whenever possible.
Engineering Considerations for Purlin Roll Forming
1. Material thickness
A purlin roll former must be configured according to the actual material thickness and steel grade. A machine designed for 1.5–2.0 mm material should not automatically be assumed to handle thicker or higher-strength steel without engineering verification.
2. Profile geometry
The forming rollers are designed around the actual C or Z purlin profile. Web height, flange width, lip dimensions and punching locations all affect roll tooling and machine configuration.
3. Punching pattern
If holes are required in the web or flange, punching position, hole size, pitch and quantity should be confirmed before machine design.
4. Forming speed
Maximum line speed is not the only performance indicator. The required speed must be evaluated together with material thickness, profile complexity, punching requirements and cutting method.
5. Profile changeover
For customers producing multiple C/Z sizes, the machine should be evaluated according to its actual size-change method rather than simply being described as an “automatic CZ machine.”
Purlin Roll Former After-Sales Support
International buyers should evaluate after-sales support before purchasing a roll forming machine.
Important services include:
Installation guidance
Remote commissioning
Operator training
Electrical troubleshooting
Mechanical troubleshooting
Spare parts support
Machine operation guidance
Long-term technical support
Beenew provides a 2-year warranty and lifetime technical support and after-sales service for its roll forming machine solutions.
Purlin Roll Former FAQ
What is a purlin roll former?
A purlin roll former is a continuous metal forming machine used to manufacture C, Z, or other structural purlin profiles from steel coils. The production line can integrate leveling, punching, roll forming, cutting, and PLC control.
What is the difference between a C purlin and a Z purlin?
C purlins have a C-shaped cross section, while Z purlins have a Z-shaped cross section. Both can be used as secondary structural members, but their geometry and connection methods differ.
Can one machine produce both C and Z purlins?
Yes. A specially designed C/Z interchangeable purlin roll forming machine can produce both C and Z profiles from one production line. The available size range depends on the machine configuration.
What thickness can a purlin roll former produce?
The standard Beenew purlin roll former published on this page is configured for 1.5–2.0 mm material. Other thickness ranges can be engineered according to the required profile, material grade, and machine design.
How many forming stations does a purlin roll former need?
The number depends on the profile geometry, material thickness, forming requirements, and machine design. Beenew's standard configuration uses 13 forming stations.
Can a purlin machine punch holes automatically?
Yes. Hydraulic punching can be integrated into the production line, and the punching dies can be customized according to the customer's required hole pattern.
Can the purlin machine automatically cut different lengths?
Yes. The PLC control system can be programmed for different finished lengths and quantities. The exact cutting accuracy and production method depend on the machine configuration.
How fast is a purlin roll forming machine?
The actual production speed depends on the profile, material thickness, punching pattern, cutting method, and machine configuration. The manufacturer should specify the actual forming speed for the customer's application rather than relying only on a generic maximum speed.
How much does a purlin roll former cost?
There is no universal price. The cost depends on profile size, material thickness, production speed, punching, cutting, automation, number of sizes, and machine configuration. A profile drawing is required for an accurate quotation.
What information is needed for a purlin roll former quotation?
Provide the purlin profile drawing, material type, steel grade, thickness, web and flange dimensions, hole pattern, finished length, required speed, and expected production quantity.
Can Beenew customize a purlin roll forming machine?
Yes. Beenew can design purlin roll forming machines according to the customer's product profile and production requirements, including C purlin, Z purlin, C/Z interchangeable, punching, cutting, and other customized configurations.
Can I inspect the Beenew factory before ordering?
Yes. Customers can request a video factory inspection or arrange a factory visit. Machine testing and production details can also be discussed before finalizing the order.
What warranty does Beenew provide?
Beenew states that its roll forming machines are supplied with a 2-year warranty together with lifetime technical support and after-sales service. The exact warranty terms should be confirmed in the sales contract.
Request a Purlin Roll Former Configuration
If you are looking for a C purlin roll former, Z purlin roll former or automatic CZ purlin roll forming machine, send us your profile drawing and production requirements.
Our engineering team can evaluate the required:
Roll tooling
Forming stations
Feeding system
Punching system
Cutting system
Drive system
PLC control
Profile changeover
Factory testing requirements
Send your profile drawing today to receive a customized purlin roll former solution and quotation.
Xiamen Beenew Machinery Co., Ltd.
No. 5, Fuming Road, Tong'an District, Xiamen, Fujian, China
Tel: +8615959271231 +8613666036199
Email: sophie@beenew-rollformer.com ivy@beenewrollformingmachine.com
Technical Review
Technical Review: Beenew Machinery Engineering Team
Subject: Purlin Roll Forming Machine Design & Manufacturing
Manufacturer: Xiamen Beenew Machinery Co., Ltd.
Machine specifications are configuration-dependent. Please verify the final technical parameters against the machine quotation and approved technical agreement before ordering.
Hot Tags: Purlin Roll Former, China, Manufacturer, Supplier, Factory
Product Tag
Send Inquiry
Please feel free to fill your inquiry in the form below. We will reply you in 24 hours.



X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies.
Privacy Policy